Hey there, if you’re new to gantry machining centers, you might think calibrating one sounds super complicated—like something only a team of rocket scientists could pull off. But let’s be real, it’s way simpler than it looks, and as someone who’s been selling and supporting these bad boys for 12 years now, I’m here to walk you through it like we’re grabbing coffee. No stuffy jargon, no confusing step-by-step that skips the “wait, why do I even do this?” parts. Gantry Machining Center
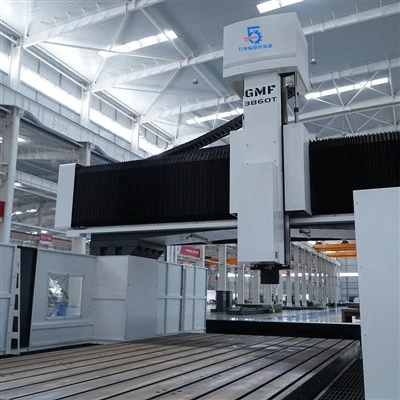
First off, let’s get on the same page: why does calibrating your gantry matter? I’ve had shops call me panicking because their 10-foot aluminum aerospace parts were coming out with 0.5mm gaps, or their mold cavities had warped edges that cost them $2k in scrap. 9 times out of 10? Bad calibration. A gantry machining center’s whole gig is moving that heavy spindle (or multiple spindles, if you’ve got a dual-gantry setup) precisely across a massive work area—way bigger than your average vertical mill. If anything’s off there, you’re not just wasting material; you’re missing deadlines, ticking off your machinists, and pouring money down the drain.
Now, before we jump in, a quick heads up: this works for most standard gantry mills, not the super custom jobbies we build for Formula 1 teams. If you’ve got one of those, give our service team a shout first. Let’s break this down into the actual work order steps, not the weird textbook ones.
First pre-calibration prep, because skipping this will make you cry later. I always tell our customers: if you rush this, you’ll end up re-doing the whole calibration in an hour. First, power the machine on and let it idle for 30 minutes. Why? Gantries are big metal beasts—parts expand and contract with temperature. If you turn it on and immediately start moving, the spindle and rails are still cold, so once they warm up mid-calibration, you’ll get a false reading. I’ve seen that so many times. Next, clear the work area of anything not nailed down—tools, scrap parts, even that half-empty energy drink your intern left there last week. Then, check the lubrication system. Gantries need constant lube on the linear ways and ball screws; if it’s low, you’ll get binding, which messes with alignment. Our machines have a little dash alert, but if yours doesn’t, check the manual (or shoot us a text, we’ll send you a quick guide). Last, set your tool offset to zero. That’s the number that tells the spindle how long your cutting tool is—if that’s off, every cut will be wrong.
Now, the main event: calibrating the three big axes: X, Y, and Z. Wait, but gantries are different from vertical mills, right? The X-axis is usually the long, side-to-side one, Y is the forward-back, and Z is up-down, but the gantry itself moves along the X-axis, while the worktable is Y. Got it? Good.
First up: X-axis straightness. This is the big one because that’s the longest travel, so any bend here ruins your whole part. The tool we use (and we recommend this to all our customers) is a precision straightedge—something like a granite straightedge, not a random ruler from your desk. Here’s how I do it in the shop: Mount a dial indicator (that’s the round tool with the needle that clicks) to the spindle, set it to zero at one end of the X-axis, say 0mm. Then jog the gantry all the way to the other end, 10 feet away. Watch the dial—if the needle moves more than 0.02mm, that means the X-axis rails aren’t straight. Now, most modern gantries have a built-in way to adjust the rail alignment, but if yours is an older model (or our entry-level ones that don’t have auto-adjust), you’ll loosen the rail mounting bolts a tiny bit, tap the rail until the dial reads flat, then tighten the bolts again. Pro tip: Don’t crank those bolts down too hard—you’ll bend the rail, and that’s a $5k repair I don’t want you to deal with.
Next, Y-axis parallelism. The Y-axis is the worktable’s travel, so this has to line up with the X-axis, otherwise you’ll cut a part that’s skewed. Same dial indicator trick, but instead of running along the X, mount the indicator on the spindle so it’s touching the side of the worktable, then jog the table along the Y-axis. If the table moves left or right as it travels, that’s parallelism off. Adjustments here are usually on the table’s mounting brackets; loosen the ones on one end, tap the table until the needle stays still, then re-torque. Easy peasy.
Then Z-axis perpendicularity. Z is the up-down, so if that’s not straight, your tools will cut at a slant—think of a hole that’s wider at the top than the bottom, which is a pain when you’re fitting fasteners. For this, we use a precision square (the granite kind again, not the plastic one you used in high school shop class). Set the square on the worktable, jog the Z-axis down so the spindle’s tool holder is touching the top of the square, take a reading on the side of the square. Then jog the Z all the way up, take another reading. If they’re off more than 0.01mm, adjust the Z-axis screws. Most gantries have a little set of screws for this, just turn them a quarter turn at a time, test, repeat. I usually do this three times to get it right—no rushing.
Wait, there’s two more things almost everyone forgets: backlash and repeatability. Backlash is that tiny gap in the ball screws when you reverse direction—like if you’re moving the machine left, then suddenly go right, it’s not instant, there’s a little play. That adds up, especially on long cuts. How to check? Use the dial indicator again: move the spindle 100mm in one direction, then move it back 100mm in the opposite. The difference between where it should be and where it is is your backlash. If it’s more than 0.01mm, adjust the ball screw nut—our service team can send you a quick video of how to do that, no fancy tools needed.
Repeatability is just how consistent the machine is. For example, if you tell it to move to position A five times, does it hit the exact same spot every time? To test that, mark a spot on the worktable, jog the spindle to it ten times, write down each dial reading. If any are off more than 0.02mm, you need to re-calibrate, or check for loose rails (weirdly, a loose bolt can cause repeatability issues even if straightness is good).
Now, let’s talk about common mistakes I see guys make. First, they skip the temperature pre-warm. I had a customer last month who calibrated his new gantry right after powering it on, and by the end of the day, his parts were off by 0.3mm. Turned out the spindle expanded 0.2mm after two hours. Lesson there: always warm up. Second, they use cheap tools. A $20 ruler won’t cut it—get a granite straightedge and dial indicator, they’re worth every penny, and we even sell them as a bundle with our machines. Third, they calibrate only once and forget about it. Oh no, you gotta do this every 3 months, or if you move the machine, or if you hit something (even a small crash into a scrap part will throw alignment off). I tell our regular customers to mark their calendars every 90 days for a quick calibration check—takes 2 hours, prevents $1k+ scrap.
Wait, what about if you have a dual-spindle gantry? Same steps, but you gotta calibrate both spindles relative to each other, so their cuts line up. That’s a tiny extra step—just mount the indicator on one spindle, touch the other, jog both, make sure they’re level. Easy, no big deal.
Now, let’s wrap this up. Calibrating your gantry isn’t some magic trick—it’s just checking three main axes, fixing tiny deviations, and doing it regularly. If you mess up, don’t sweat it—we’ve all been there. And hey, if you don’t want to do it yourself? Our service team can come out and do a full calibration for you, or even walk you through it over a screen share while you do it. No big hassle.

If you’re in the market for a gantry machining center that’s easy to calibrate (we build ours with built-in adjustment tools so you don’t have to mess with weird bolt tightness), or you need support for the one you already have, hit us up to chat. We’ve been helping shops for years, and we’ll hook you up with whatever you need—whether that’s a new machine, calibration help, or even just tips to keep yours running smooth. No sales pitches, just straight talk.
CNC Gantry Boring Mill References
- Machinist’s Guide to Gantry Machining Center Alignment and Calibration, Industrial Manufacturing Association, 2021
- Precision Calibration for Large-Scale CNC Machine Tools, Journal of Manufacturing Engineering, Vol. 19, No. 3, 2019
- Operator’s Manual: Gantry Machining Center Setup and Maintenance, Techno Machine Tools Inc., 2022
- Temperature Compensation in CNC Machine Calibration, International Journal of Machine Tools and Manufacture, Vol. 56, 2020
5Axis (Shandong) CNC Equipment Co., Ltd.
As one of the most professional gantry machining center manufacturers and suppliers in China, we also accept customized orders. Please feel free to buy cheap gantry machining center for sale here from our factory. For price consultation, contact us.
Address: No.2000, Beixin West Road, Jinghe Street, Tengzhou City, Zaozhuang City, Shandong Province
E-mail: summer@good5axis.com
WebSite: https://www.china5axis.com/
