Hey there, it’s Jake from [Your Company Name]—today I wanna break down something that everyone in the PET injection molding world obsesses over, but hardly anyone explains simply: the barrel. If you’ve ever stood next to a running PET machine, you’ve probably seen that big, metal cylinder wrapped around heaters and surrounded by that motor hum, right? Most people just call it “the barrel” and think, “Cool, it holds plastic,” but dude—this part is basically the heart of your whole molding process. Mess up how your barrel works, and you’re not just throwing away PET resin; you’re messing up part quality, cycle times, and even your bottom line. Let’s get into it, no boring textbook jargon, promise. PET Injection Molding Machine
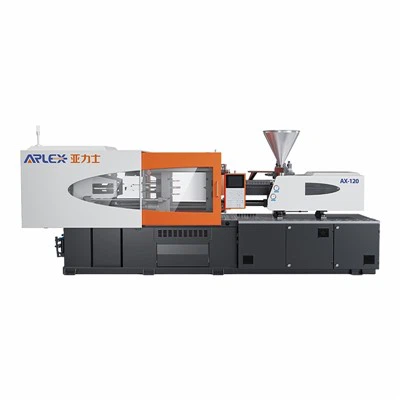
First, let’s start with what a barrel actually does, step by step, because if you skip the basics, you’ll never get why it’s so important. When you load PET resin into your machine, that stuff comes in little pellets, right? They’re hard, opaque, and solid at room temp—totally not the goopy plastic you want for a preform or bottle cap. The barrel’s job is to turn those solid pellets into a uniform, molten mass that’s 100% consistent in temperature and texture. But it doesn’t just melt them—this is where so many new operators go wrong. See, PET is a finicky material; it’s hygroscopic, meaning it sucks moisture out of the air like a sponge. If you don’t dry it first, that moisture will boil when it hits the hot barrel, causing bubbles in your preforms—defects that make them unusable, no matter how good your mold is. Good barrels are designed with feed zones that work with your dryer to move those dry pellets evenly, so no wet spots sneaking through.
Wait, let’s get specific about the structure of a typical PET barrel, ‘cause not all barrels are created equal. Most barrels have three main sections, right? The feed zone, the transition zone, and the metering zone. The feed zone is the back part, where pellets get dropped in. This part is cooled, actually—crazy, right? If the feed zone got too hot, the pellets would start melting too soon, clump together, and jam up the screw. That’s a super common issue; I’ve had customers call me at 2 a.m. ‘cause their feed zone overheated, pellets melted into a solid block, and the screw locked up. We had to send a tech out the next day, and they lost 3 hours of production. Total headache, all ‘cause they didn’t realize the feed zone needs to stay cool, not hot.
Then the transition zone is where the magic happens. This is where the heaters crank up, and the screw starts moving the pellets forward, compressing them as they go. PET needs to be heated to a specific range—usually around 260°C to 285°C (that’s like 500°F to 545°F, for my imperial folks)—and if the barrel’s heating elements are uneven, you’ll get hot spots in the molten PET. Hot spots make PET degrade, right? Degraded PET gets yellow, brittle, and loses its clarity—total death for water bottles or soda preforms, where clarity is everything. That’s why we build our barrels with evenly spaced heating bands, and we calibrate them before they ship—no guessing if the middle of the barrel is the same temp as the end.
The last section is the metering zone, which is where the molten PET gets mixed to that perfect consistency before it shoots into the mold. This is where the screw does its work—shearing the plastic, making sure it’s uniform, and dosing exactly how much molten PET you need for each preform. If your barrel’s metering zone isn’t precise, you’ll get short shots (not enough plastic, so the preform’s missing the neck) or overpacked parts (too much plastic, so the neck is too big or the base is warped). We’ve had customers switch to our barrels and cut their short shot rate by 40%—that’s thousands of good parts more every shift, just from a better barrel.
Now, here’s something most people don’t talk about: barrel wear. PET is actually pretty abrasive, right? It has little crystal structures in the pellets that rub against the screw and the barrel every time you cycle the machine. Over time, that wear makes the barrel’s inner diameter wider, and the screw doesn’t fit as tight. When there’s too much gap between the screw and the barrel, molten PET slips past instead of moving forward—you get inconsistent dosing, cycle times get longer, and you waste resin. We see this all the time with used machines that have cheap barrels; after a year or two, they’re throwing away 10-15% of their PET resin every run. Our barrels are made with wear-resistant materials—we use nitrided steel or even bimetallic liners for high-volume operations—so they last 2-3x longer than standard barrels. I had a customer running 24/7 making 500ml water bottle preforms; their old barrel wore out in 18 months, switched to ours, and they hit 4 years of consistent runs before they even needed to think about replacing it. That’s not just saving on barrel costs—that’s saving them tens of thousands a year in wasted resin and downtime.
Wait, let’s also touch on barrel temperature control, ‘cause this is make or break for PET. PET is way more sensitive to temperature than, say, PP or HDPE. If your barrel’s temp is off by even 5°C, you’ll notice a difference. Too low, and the PET is too thick to flow into the mold, leading to incomplete preforms. Too high, and you get that degradation I mentioned earlier—yellow parts, maybe even fumes that mess up your machine’s electronics. A lot of budget barrels use basic thermocouples that are spaced out, so they don’t track temp accurately. Our barrels use high-resolution thermocouples every 2 inches along the barrel, so we can adjust heating in real time, keeping that temp dead on. We had a customer who was getting 8% reject rate on preforms ‘cause their old barrel’s temp was 7°C too high at the metering zone. Switched to our barrel, and their reject rate dropped to less than 1%—that’s a game-changer for their production.
Another thing: the barrel’s design for screw compatibility. If you’re running a PET machine, you’re using a screw specifically for PET, right? The barrel has to match that screw’s L/D ratio (length to diameter) perfectly. A PET barrel needs a longer length than, say, a nylon barrel, ‘cause PET needs more time to melt and mix evenly. Too short a barrel, and you’ll get unmelted pellets in the molten plastic—those are called “fish eyes” in the part, and they make the bottle look cheap, or even fail pressure tests. We design all our barrels to pair with industry-standard PET screws, but we also custom-build them for customers with specific needs—like if they’re running rPET (recycled PET), which is even more abrasive, so we beef up the liner even more. rPET is huge right now, and a lot of operators don’t realize that standard barrels can’t handle it—they wear out way faster, leading to more downtime. Our bimetallic barrels are made for rPET, so our customers can run recycled resin without worrying about barrel wear.
Let me throw in a real quick story to make this concrete. A few months back, I got a call from a small bottling company in Ohio. They had 3 old PET injection molding machines, all with generic barrels they bought cheap online. They were running preforms for 2L soda bottles, and they were losing about $12k a month in rejected parts, resin waste, and unplanned downtime. Their old barrels were wearing unevenly—one side was wider than the other, so the screw would wobble, leading to inconsistent dosing. We sent them a quote for our standard PET barrels, and they hesitated at first ‘cause they thought it was more expensive. But after we ran a quick audit, we showed them that switching would save them over $18k a month, once they factored in less waste, fewer rejects, and less downtime. They took the plunge, and 3 months later, they called me back saying they’d already paid for the new barrels and were on track to save over $70k a year. That’s not a sales pitch—that’s what a good barrel does.
Now, if you’re running PET injection molding, you might be thinking, “Okay, so a good barrel is important, but how do I know if mine is working right?” Let’s do a quick checklist. First, check your reject rate—if it’s over 2% for consistency or clarity, that’s a red flag, probably barrel temp or wear. Second, watch your cycle times—if they’re getting longer without changing settings, that’s usually worn barrel/screw. Third, check your resin consumption—if you’re using more than your baseline to make the same number of parts, that’s wasted plastic from slippage in a worn barrel. If you’re noticing any of these, don’t just keep running and hoping it fixes itself—tune up your barrel, or upgrade if you need to.
Look, I know when you’re in the thick of production, it’s easy to fixate on the mold or the robot arm, ‘cause those are the parts you see making parts. But the barrel is the workhorse that makes all that happen. It’s the reason your pellets turn into molten plastic, the reason your parts are consistent, the reason you’re not throwing away money on bad resin.

If you’re tired of dealing with high reject rates, frequent barrel breakdowns, or wasted PET resin, hit us up to talk shop. We’ve been building PET barrels for over a decade, so we know the ins and outs of every kind of machine, every resin type, every production need. We don’t sell one-size-fits-all barrels—we’ll work with you to figure out exactly what you need, whether you’re running a small 4-cavity machine for local bottled water or a high-volume 48-cavity line for a national soda brand. Don’t let a bad barrel kill your production—reach out, and let’s get your process running smoother.
PET Injection Moulding Machine References:
- Rosato, D. V., & Rosato, M. G. (2000). Injection Molding Handbook. Kluwer Academic Publishers.
- Giles, H. F., Wagner, J. R., & Mount, E. M. (2004). Extrusion: The Definitive Processing Guide and Handbook. William Andrew Publishing.
- ASTM D638-14, Standard Test Method for Tensile Properties of Plastics. ASTM International.
Ningbo Yalishi (Arlex) Plastic Machinery Co., Ltd.
Address: No.63, Huangsu East Road, Industrial Zone, Dongqian Lake Tourist Resort, Ningbo, Zhejiang Province
E-mail: leo@arlex.cn
WebSite: https://www.arleximm.com/
