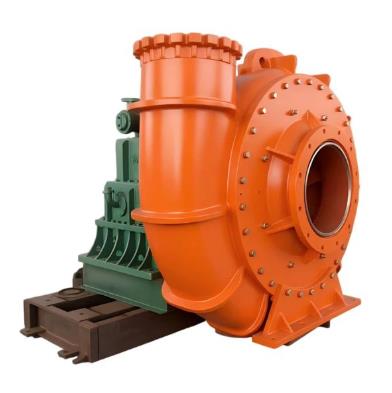
If you’ve ever stood beside a processing plant or mining site on a hot shift, you know a slurry pump doesn’t just move mud and mineral sludge—it’s the backbone that keeps the whole operation running. As someone who’s spent 12 years working with slurry pumps, first as a field service tech and now as part of the team at our pump supply company, I’ve seen firsthand how a pump that works flawlessly one month can grind to a halt the next, all because of small, easy-to-miss factors no one talks about in basic pump manuals. Most operators blame “bad parts” or “cheap assembly” when performance dips, but more often than not, it’s a mix of conditions that surround the pump, not the pump itself, that make or break how well it works. Today, I want to break down those real-world factors, from the stuff you can see on a daily walkthrough to the lab-tested properties of the slurry, that actually affect performance—and how we help customers fix them before they lead to costly downtime. Slurry Pump
First, let’s talk about the slurry itself, because it’s not just “water with rocks in it.” This is the biggest variable I see, and it trips up even seasoned superintendents. Slurry density, measured in solids by weight, changes daily in most operations. A gold mine might run 40% solids on Monday, but if they push a batch of unprocessed ore through on Wednesday, that jumps to 55%—suddenly, the pump’s impeller is working 30% harder to move the thicker mix. I learned this the hard way early on: a copper mine client once thought their new pump was defective because it couldn’t hit the required flow rate, but when we tested the slurry, it was 58% solids, way above the pump’s design spec for that application. Slurry particle size and shape matter too. Angular, sharp quartz particles wear down impellers and casings twice as fast as rounded, smooth ones, and if you’ve got a mix of fine silt and large rocks (called a “multimodal” gradation), those big rocks can get caught in the volute, causing cavitation and shifting the pump’s efficiency curve. Even the viscosity of the base liquid counts—if you’re moving slurry through a tailings pond in cold weather, water gets thicker, and that extra viscosity reduces flow by as much as 15% without any changes to the pump. We always tell customers: test your slurry daily, don’t just go by the weekly average. That one small step will eliminate half the performance surprises.
Next, the pump’s design and sizing. I know, it seems obvious, but you’d be shocked how many operations run a pump that’s either too big or too small for their current needs. Oversized pumps are a common mistake: some plant managers buy a pump with extra capacity “just in case,” but oversized pumps run at part load most of the time, which makes them inefficient, generates more heat, and wears out seals faster. A gravel pit I worked with did this—their original pump was sized for a 200 GPM flow, but they bought a 300 GPM unit thinking it would last longer. After six months, the pump’s energy bill was 25% higher than it needed to be, and the impeller was eroded unevenly because it was spinning too fast at low load. Undersized pumps are even worse—they can’t move the required slurry volume, leading to overflow, bottlenecks in the processing line, and constant overload on the motor. It’s not just flow rate either; the impeller type and material matter. Closed impellers work best for fine, low-abrasion slurry, while open or semi-open impellers are better for larger particles that would clog a closed design. Hard metal impellers are standard for high-wear applications, but if you’re moving mild slurry, a high-chrome impeller is overkill and adds unnecessary cost. We work with every customer to map their exact slurry specs and flow needs to the right pump, no over-sizing, no under-sizing, just what works for their unique operation.
Then there’s the installation and piping setup, which is almost entirely overlooked until something breaks. I can’t tell you how many times I’ve showed up to a site where the pump is installed on an uneven foundation, or the suction pipe is too small, leading to cavitation. Cavitation is when low pressure at the impeller inlet causes bubbles to form, then collapse violently as they move to higher pressure zones, eroding metal and causing the pump to lose flow. A common cause of cavitation is a suction pipe that’s too narrow, or has too many sharp elbows, or a lift that’s too high (meaning the pump has to pull slurry up a long distance from the sump). Last year, a cement plant called us because their pump was making a loud rattling noise and losing 20% of its flow. When we looked at the suction line, it was 2 inches smaller than the pump’s required inlet size, and there were three 90-degree elbows right at the pump inlet. We redesigned the suction line to match the inlet size, replaced the elbows with long-radius ones, and the cavitation went away immediately. Even the alignment of the pump and motor matters—if they’re even a millimeter off, you’ll get unnecessary vibration, which wears out bearings and seals fast. We include on-site installation reviews as part of our pump supply packages, because we know a pump is only as good as how it’s put in.
Operating conditions and maintenance round out the list, and these are the factors that change every shift, not just over months. Operating speed is a big one—running a pump faster than its design RPM increases wear exponentially, not linearly. Double the speed, and wear goes up eight times, because the particles hit the impeller with more force. Many operators crank up the speed when flow drops, thinking that will fix it, but that just accelerates wear and leads to a pump failure a few weeks later. Instead, they should check if the slurry density has changed, or if there’s a clog in the suction line. Maintenance is another make-or-break factor. A pump that’s supposed to run 24/7 will wear parts over time, and if you don’t replace impellers or seals before they’re completely worn, performance drops. I saw a mining operation go three months without replacing their impeller, even though the wear rate chart said it should be changed every six weeks. By the time they finally called us, the pump’s flow was down 35%, and the casing had a ¼-inch groove worn into it, so they had to replace the whole pump, not just parts. Regular, scheduled checks—looking at vibration, pressure, flow rate, and seal condition—catch these issues early. We provide customized maintenance checklists for every pump we supply, tailored to their slurry’s abrasion and density, so they don’t have to guess when to replace parts.

Last, ambient and site-specific conditions that you wouldn’t expect. Extreme temperatures affect both the slurry and the pump’s components. In cold climates, pump seals and gaskets can harden and crack, leading to leaks that reduce performance. In hot, dusty environments, dust can get into the motor’s cooling fins, making the motor overheat and reducing its power output. A quarry in Arizona had this problem: their pump motor was in a dust-filled enclosure, and every month they had to shut down to clean the fins, which cut production by 5% each time. We helped them install a filtered enclosure for the motor, and that shut down went away. Even altitude matters—at higher elevations, atmospheric pressure is lower, which increases the risk of cavitation because the pump has to work harder to pull slurry in. We adjust pump sizing for altitude, adding a small buffer to the suction pressure to avoid cavitation, something most generic pump suppliers don’t account for.
Sand Pump At the end of the day, a slurry pump’s performance isn’t just about the pump itself—it’s a combination of the slurry you move, how you size and install the pump, how you operate and maintain it, and even the weather at your site. As a pump supplier, my team’s job isn’t just to sell you a pump and walk away. We work with you through every step: testing your slurry to make sure we size the right pump, reviewing your installation to avoid common pitfalls, and providing the tools and checklists to keep it running smoothly. If you’re dealing with a pump that’s underperforming, having unplanned downtime, or just want to optimize your operation for lower energy costs and longer pump life, don’t guess at the solution. Reach out to our team for a consultation—we’ll walk through your site, test your slurry, and help you get the most out of your slurry pump.
References
- Karassik, I. J., Messina, J. P., Cooper, P., & Heald, C. C. (2008). Pump Handbook (3rd ed.). McGraw-Hill.
- Ministry of Education, Culture, Sports, Science and Technology. (2017). Slurry Pump Wear and Performance Optimization. Industrial Science and Technology Press.
- American Water Works Association. (2020). Guidelines for Slurry Pump Installation and Operation. AWWA.
- Sanders, M. (2019). “Factors Influencing Slurry Pump Efficiency in Mineral Processing Plants.” Journal of Process Technology, 42(2), 112-127.
Shijiazhuang Ruite Pump Co., Ltd.
As one of the most professional slurry pump manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please feel free to buy durable slurry pump for sale here from our factory. Quality products and reasonable price are available.
Address: Majuan village, Nandong town, Gaocheng, Shijiazhuang, China
E-mail: info@ruitepump.com
WebSite: https://www.rtslurrypumps.com/
