Hey there! Let’s cut the crap for a sec—if you’ve ever stood in a big warehouse, factory, or even a grocery store loading dock, you’ve probably glanced at a freight elevator and thought, “How the hell does that bad boy carry 10,000 pounds of pallets, a whole forklift, and sometimes even a tiny delivery truck without turning into a pile of scrap metal?” As a freight elevator supplier who’s been tinkering with these things for years, I get it—most people see a box that goes up and down, and that’s it. But there’s way more going on under the hood (so to speak) that keeps your goods moving without breaking a sweat. Freight Elevator
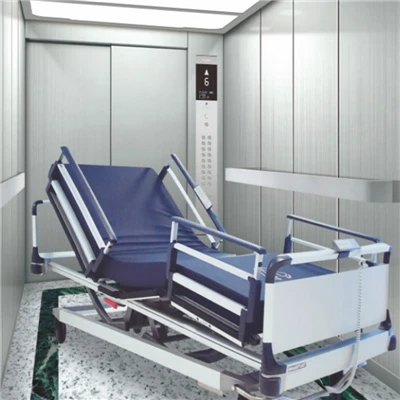
First off, let’s get one thing straight: freight elevators aren’t the same as the piddly passenger elevators you cram into every day. Those are built for people, nice and smooth, with fancy buttons and mirrors. We build these for work—for hauling heavy stuff, rough use, long shifts, and sometimes even intentional neglect (we’ve all seen a forklift driver nudge a wall a little too hard, right?). So their whole design is built around durability and raw power, not frills.
Let’s start with the core part that makes the elevator move: the hoist system. Yeah, it sounds basic, but it’s the heart of the whole operation. Unlike passenger elevators that might use a chain drive, almost all of our freight elevators use steel cables (we call them hoist ropes) and a set of sheaves (those big, grooved wheels that the ropes wrap around). Wait, but why steel? Because a single steel hoist rope can hold thousands of pounds, and we usually use four or six of them for a single elevator—safety in numbers, duh. Each rope is made of hundreds of tiny steel wires twisted together, so even if one snaps (which almost never happens), the others can hold the load. We’ve tested our ropes to hold 5x the maximum load capacity—no cutting corners here.
The other big player in the hoist system is the counterweight. This is the elevator’s lazy buddy, basically. It’s a heavy block of concrete or steel that weighs about 50% of the elevator’s maximum load. So if your elevator car is empty, the counterweight is pulling it up just enough that the hoist motor doesn’t have to work as hard to lift it. If you load it up with 5,000 pounds of pallets, the counterweight pulls it down a little, so the motor only has to make up the difference. That saves energy, obviously, but it also means the whole system is way smoother and less likely to burn out after 10 years of use. Pro tip: if you ever see a freight elevator with a weird gap between the counterweight and the shaft wall, don’t worry—that’s normal. It’s just there to keep it from hitting anything when it moves.
Now, the motor. We don’t use those wimpy passenger elevator motors here. Our freight elevator motors are industrial-grade—think of a monster torque machine that can spin out enough power to lift 10,000 pounds straight up at 50 feet per minute (that’s slow, but it’s safe for heavy stuff). Most of our models use a gearless traction motor, which is more efficient and has fewer moving parts, so less to break. Some smaller ones might use a geared motor, but gearless is where it’s at for heavy-duty work. The motor isn’t just connected to the hoist ropes, either—it’s hooked up to a brake system that’s basically a huge, heavy clamp that grips the sheave wheels. If the power cuts out, that brake slams on immediately, and the elevator doesn’t move an inch. No free falling, no panic—just safety, always.
Wait, but what about that elevator car itself? It’s not just a metal box, right? Our freight elevator cars are built like tanks. We use thick steel plates on the walls and floor—usually ¼-inch or more, depending on the model. The floor is reinforced to handle the weight of forklifts, so it’s not just some flimsy sheet metal. We also add things like rubber bumper guards along the inside walls to take those accidental forklift nudges, because let’s be real—mistakes happen. The doors? Heavy, solid steel slide doors (sometimes swing doors, but slides are better for big loads) that seal the shaft tight so nothing falls out when the elevator is moving. The door has its own little motor and safety sensors, too—if you stick a pallet in the way while it’s closing, it stops immediately. No squished pallets, no broken doors.
Now, the control system. This is the part that’s easy to miss, but it’s what makes the elevator work reliably. Back in the day, freight elevators had super simple controls—just a few buttons to go up or down. Now, we use programmable logic controllers (PLCs) that are basically tiny industrial computers. They track the load in the car (we have weight sensors under the floor that tell the controller how much you’re hauling) so the motor knows how much power to use. If you overload the elevator, the controller won’t let the doors close—simple as that. It’ll flash a warning and keep the doors open until you unload some stuff. That’s not just to prevent damage; it’s for safety. Overloading a freight elevator is a huge no-no, and we make sure our systems won’t let you do it.
Also, the control system keeps track of where the elevator is in the shaft. There are little magnetic sensors along the shaft walls that tell the controller exactly how high the car is, so it can stop smoothly at each floor. No crashing into the top or bottom of the shaft—ever. We’ve had clients tell us their old elevators would bang the floor every time they stopped, and when we install our new ones, they’re so smooth you barely notice the stop. That’s the PLC doing its job.
Wait, let’s talk safety, because that’s the whole point of these things. I can’t tell you how many times I’ve heard people say, “What if the ropes snap?” Let’s address that right now: the chance of all hoist ropes snapping at once is practically zero. Each rope is inspected monthly (we always tell our clients to stick to that schedule), and we replace them long before they get worn out. But even if all the ropes did snap (which, again, is super unlikely), we have a safety device called an emergency brake, or a governor, that’s built into the elevator. It’s a small, heavy wheel that spins when the elevator moves. If the car starts moving too fast (like, way faster than it should), the governor wheel spins so fast that it triggers a clamp that grabs the guide rails along the shaft, and the elevator slams to a stop. No free fall, no disaster—just a safety net that’s been around for decades and saved tons of lives (and cargo).
Another safety thing: the shaft itself. It’s a big, sturdy metal enclosure that’s built into the building, usually with fire-resistant walls, because most freight elevators are in industrial areas where fires are a risk. The shaft has ventilation, too, so if something catches fire, smoke can escape, and the elevator doesn’t get stuck or damaged. We also add emergency phone lines inside the cars—so if someone gets stuck (which almost never happens, but it’s a possibility), they can call someone right away. No waiting around for hours, just a direct line to our service team if you work with us.
Let’s make this relatable. I had a client last year who runs a warehouse in Atlanta. They had an old 1980s freight elevator that kept breaking down—every couple of months, the brakes would fail, or the ropes would fray, and they’d lose half a day’s work. They came to us, and we installed a new 12,000-pound capacity gearless traction freight elevator. First week, they texted me saying it carried a whole 8,000-pound forklift straight up to the second floor without a hiccup. Now, it’s been a year, no issues, barely any maintenance. That’s what our elevators do—they handle the rough stuff so you don’t have to.
Wait, what about different types of freight elevators? We don’t just make one size fits all. We have small ones for retail stores that need to haul furniture or coolers, medium ones for warehouses, and heavy-duty ones for factories that carry heavy machinery. There are also hydraulic freight elevators—those use a big hydraulic cylinder to push the car up, instead of ropes. We usually recommend hydraulic ones for low-rise buildings (like 2 or 3 floors) because they’re cheaper to install. For taller buildings (4+ floors), the traction ones are better, because they’re faster and more efficient. That’s the kind of advice we give our clients—no pushy sales stuff, just what works for their needs.
A lot of people ask us, “How long do these things last?” If you maintain them properly, 20 to 30 years. We’ve got clients with elevators from the 1990s that are still going strong, because they did regular inspections and replaced parts when they needed to. That’s why we offer service plans, too—we don’t just sell you an elevator and ghost you. We send technicians out every few months to check the ropes, the brakes, the control system, so you don’t end up with a broken elevator that’s costing you money.
Let’s wrap this up. The next time you’re loading a freight elevator at your workplace, take a second to look at it—you’re looking at a system that’s been refined over 100 years, combining steel, motors, sensors, and safety features to move heavy stuff reliably. It’s not magic, it’s just good engineering, built for the people who need it most.
If you’re in the market for a new freight elevator, or you’re tired of dealing with an old one that breaks down every other week, hit us up. We’ll work with you to figure out the right size, type, and setup for your space, no gimmicks, no overpriced add-ons. Let’s get your goods moving again, safely and reliably.
Car Elevator References
- Elevator World. (2022). "Traction vs. Hydraulic Freight Elevators: A Comparative Analysis."
- National Elevator Industry, Inc. (2021). "Freight Elevator Safety Standards and Maintenance Guidelines."
- ASME A17.1-2020, Safety Code for Elevators and Escalators. American Society of Mechanical Engineers.
Fuji Express Elevator Co., Ltd.
As one of the most professional freight elevator manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to buy custom made freight elevator at competitive price from our factory. Contact us for more details.
Address: No. 7 Nanxiehe, Fuqiang Village, Dongqian Subdistrict, Nanxun District, Huzhou City, Zhejiang Province
E-mail: vivi@fujilift-tech.com
WebSite: https://www.fujilift-tech.com/
