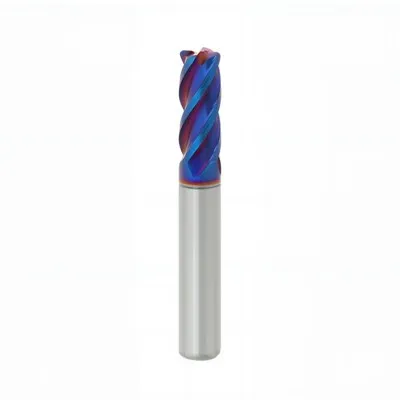
If you’ve ever spent time in a machine shop—whether running a CNC machine, troubleshooting a part, or just overhearing a machinist vent about a botched finish—you’ve probably heard someone ask, “What kind of surface roughness can I actually get with a flat end mill?” It’s not a trick question, but it’s one that’s way more nuanced than just “it depends.” As a flat end mill supplier, I hear this every single day from customers ranging from hobbyists building a drone frame to aerospace shops cranking out turbine blades. Most people assume surface roughness is a random “good or bad” thing, but once you break it down, it’s totally predictable—if you know what to look for. First, let’s get one thing straight: surface roughness (Ra, Rz, all those numbers) isn’t the same as surface finish. Ra is the average deviation of peaks and valleys from a perfectly flat surface, measured in microns or micro-inches, and it’s the most common spec shops use. Rz is the total vertical distance from the highest peak to the lowest valley, which is useful for things like fluid flow parts, but Ra is the go-to for most general work. Now, what can you actually hit with a flat end mill? Let’s start with the baseline, no fancy tricks. If you’re just using a generic high-speed steel (HSS) flat end mill, running at standard speeds for aluminum or steel, you’re looking at an Ra of like 3.2 to 6.3 microns (that’s ~125 to 250 micro-inches). That’s the finish you’d get on a bracket that doesn’t need to look pretty, just hold tight. But if you’re upgrading to a solid carbide flat end mill—way more common now because it holds an edge way better—you can easily drop that to 0.8 to 3.2 microns (~32 to 125 micro-inches) with a single pass, no extra steps. I’ve had a customer machining aluminum heat sinks for LED lights hit 0.4 microns (~16 micro-inches) just by dialing in their feeds and speeds, no polishing, no secondary operations. Wait, hold on—can you really get that smooth with a flat end mill? A lot of people think you need a ball nose or a finish mill for that, but flat end mills are way underrated for precision work if you pick the right one. Now, why does it vary so much? It’s not magic, it’s just variables that everyone overlooks. Let’s break down the big ones, since this is stuff that comes up in my inbox weekly. First, the end mill’s geometry. If your flat end mill has 2 flutes, that’s gonna leave bigger feed marks than a 4-flute or 6-flute, right? The formula is basically: feed per tooth times the number of flutes equals the feed rate, and smaller feed per tooth = smaller valleys. But that’s only if the tool is sharp. A dull end mill will rub instead of cut, leaving a smudged, uneven surface—you can’t polish that up later, it’s just heat damage. I see so many guys try to stretch a flat end mill’s life too far and wonder why their finish is garbage. Then there’s the material you’re cutting. Aluminum is way easier to get smooth than stainless steel, for example. Aluminum chips cleanly, so no built-up edge (BUE) on the tool, which is a huge roughness killer. Stainless has that nasty tendency to gum up the cutting edges, so you’ll get tiny, uneven bumps if you don’t use the right coating. Coating! That’s another big one. Uncoated carbide is fine for roughing, but if you want a smooth finish, you need something like TiAlN or diamond-like carbon (DLC). DLC coatings are super smooth themselves, so they reduce friction between the tool and the part, which eliminates those tiny drag marks. I have a batch of DLC-coated flat end mills that my customers swear get 0.2 microns (8 micro-inches) on aluminum— that’s almost mirror finish with a flat end mill, no hand polishing required. Next up: machine setup and programming. If your CNC machine has any runout in the collet, that means the end mill is wobbling a little as it spins. Even a tiny runout (like 0.02 mm) will make uneven cuts, so your surface roughness jumps way up. Also, feed rate—too fast, and you’re not cutting clean, you’re chipping the material; too slow, and you’re rubbing. For finish passes, you want a lighter cut too—like 0.1 to 0.2 mm depth of cut, not 2 mm. I see a lot of machinists use the same settings for rough and finish passes, and wonder why their part looks like it was milled by a beginner. Now, let’s talk about what’s actually achievable for different use cases, because that’s what most people care about. If you’re a hobbyist making a custom sign or a wooden fixture, 6.3 to 12.5 microns (250 to 500 micro-inches) is totally fine—you can even get that with an HSS end mill, no problem. If you’re a maker making a drone arm or a bracket, 1.6 to 3.2 microns (63 to 125 micro-inches) is standard, and that’s where solid carbide end mills shine. For industrial parts—like medical implants, hydraulic valves, or optical mounts—you’re looking at 0.4 to 1.6 microns (16 to 63 micro-inches). Yeah, that’s possible with a flat end mill, as long as you’re using a high-quality tool, a rigid machine, and the right programming. Wait, but can you get below 0.4 microns? That’s where it gets tricky. You might see some labs or high-end aerospace shops hitting 0.1 to 0.2 microns (4 to 8 micro-inches) with a specialized flat end mill, but that’s not something a typical shop can do every day. It requires a super rigid machine, absolutely zero runout, very high spindle speed, and sometimes a secondary operation like a light polish or a tumble. Most of the time, you don’t even need that spec—paying for that level of finish is overkill for most parts. I always tell customers: pick the lowest Ra you need, not the highest you can get, because it’ll save you time and money. A common mistake people make is thinking a higher Ra number is better, but no—Ra is the average, so smaller numbers mean smoother. If you’re machining a part that needs to seal, like a hydraulic piston, you need low Ra to stop leaks. If it’s a structural bracket, a higher Ra is totally fine, even if it looks a little rough. Let’s also address the myths out there. A lot of guys say “flat end mills can’t do smooth finishes, only ball mills” but that’s outdated. Ball mills have round edges, so they can cut complex curved surfaces, but for flat faces, a flat end mill gives a more consistent finish. Ball mills leave tiny round marks, while flat end mills leave straight feed marks that are easier to clean up, and you don’t have to do multiple passes like you do with a ball mill. Another myth: “you need a 5-axis machine to get a smooth finish.” No, a good 3-axis CNC with a properly set up collet will get you way better results than a cheap 5-axis with loose tooling. Now, as a flat end mill supplier, I’ve seen a lot of customers switch from generic budget end mills to our precision ones and cut their surface roughness in half, without changing their machine or their process. It’s not magic, it’s just a tool that’s designed to hold its edge and have a consistent, sharp cutting edge—way different from the $1 end mill you buy at the hardware store for a one-time project. The big takeaway here: surface roughness with a flat end mill isn’t a fixed number. It’s a range, controlled by tool quality, geometry, machine setup, and material. You’re not limited to a rough, industrial finish if you pick the right tool. If you’re currently dealing with inconsistent finishes, dull tools that wear out after 10 parts, or you’re not sure what Ra spec you actually need for your next project, hit us up. We’ve worked with shops from hobbyists to large OEMs to help them pick the right flat end mill for their material and finish requirements, no confusing jargon, no overpriced tools you don’t need. Don’t guess on your tooling—get the right info to get the finish you want, without wasting time or money. Flat End Mill
Internal External Threading Inserts References
- "Surface Roughness Prediction in Milling Operations," Journal of Manufacturing Processes, 2018.
- Machining Data Handbook, 11th Edition, Manufacturing Engineering Society International, 2021.
- Tool Geometry and Surface Finish in End Milling, SME International, 2020.
- "Effect of Cutting Parameters on Surface Roughness of Aluminum Alloy Milling," International Journal of Machine Tools and Manufacture, 2019.
Small Craftsman (Shandong) Machine & Tools Co., Ltd.
Small Craftsman (Shandong) Machine & Tools Co., Ltd. is one of the most experienced flat end mill manufacturers and suppliers in China, also supports customized service with low price. Please feel free to buy bulk high quality flat end mill in stock here from our factory. Contact us for pricelist.
Address: No.9 Quanxin Rd., Sishui Economic Developing Zone, Jining, Shandong, China.
E-mail: 6196@ocutchina.com
WebSite: https://www.ocutooling.com/
